Sorbitol Solution 70%
Product Description
Sorbitol Solution 70% Manufacturer and Supplier
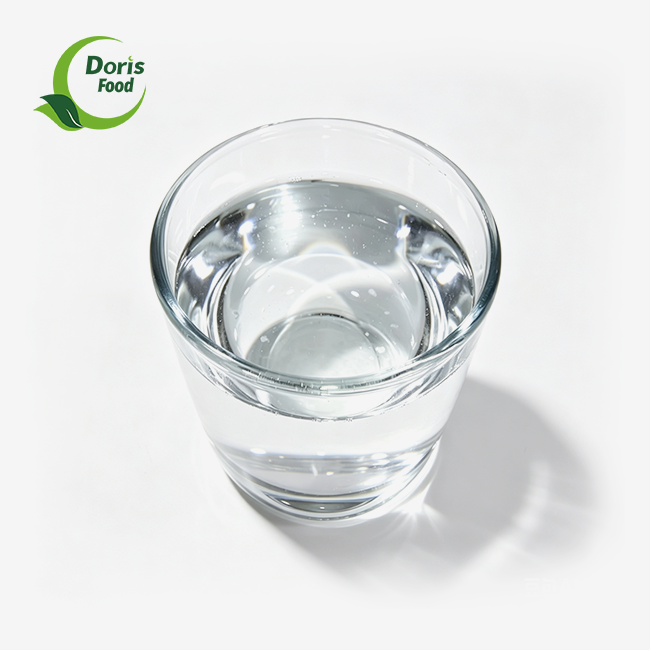
We've been providing 97 industrial food makers around the world with a wide range of 208 premium products since 2017. Our Sorbitol Solution 70% is a clear, colorless syrupy liquid that has about 70% D-Sorbitol in a stable watery form. It is made by hydrogenating high-purity glucose with a catalyst.
Our solution is very hygroscopic and chemically stable, with a specific gravity range of 1.285 to 1.315 and a pH range of 5.0 to 7.5. It has about 60% of the sweetness of sugar and better qualities for keeping water in and preventing crystallization. Our approved quality systems, which include FDA, ISO, HALAL, KOSHER, and FSSC certifications, make sure that every batch meets the highest standards for food safety around the world.
Why Choose Us?
Fast Customization & Delivery
When making food, time is important. Customized recipe development takes seven days, and assembly takes about fifteen days. You'll never have to worry about production delays because we keep certain goods in stock.
One-Stop Procurement Advantage
Why deal with several suppliers? All of our 208 food items are in one place, so you can combine your orders and make buying easier. Some clients buy up to 28 different kinds of ingredients from us, which cuts down on prices and the work of managing suppliers.
Global Logistics Excellence
The goods get to you on time and safely. We offer a full range of shipping services, such as air freight, sea freight, and land transportation. Our service for filling mixed containers and quick help with customs clearance make sure that deliveries go smoothly all over the world.
Technical Support That Works
Not only are you buying goods, but you're also getting a skilled partner. Our skilled staff can help you make the best soups, baked goods, drinks, sweets, and meat processing ingredients by giving you professional application advice.
Certified Quality You Can Trust
You can always count on certified quality. Quality isn't up for discussion. Our Sorbitol Solution 70% complies with USP-NF, EP, and FCC standards. We ensure steady quality that meets your legal needs in all areas thanks to our seven important approvals, such as BRC and RSPO.
Competitive Pricing Without Compromise
We offer cost-effective options without lowering quality by having good ties with our suppliers and running our business efficiently. You can get pharmaceutical-grade materials at costs that are competitive for businesses.
Sorbitol Solution 70% Key Advantages
Superior Moisturizing Performance
The food you sell stays fresh longer. Our method gives baked goods, sweets, and prepared foods great humectancy that keeps them from drying out. It keeps the balance of wetness even in places with low humidity.
Low Sweetness with Clean Taste
You get useful benefits without too much sugar. Because it is 60% as sweet as sugar, it gives you exact control over the flavors in your recipes while also giving them the mouthfeel and body you want.
Effective Anti-Crystallization Property
Get rid of the rough surfaces. The solution keeps sugar from crystallizing in frostings, fondants, and sweets, so they stay smooth for as long as they're stored.
Outstanding Stability & Compatibility
It works well with the formulas you already have. Our Sorbitol Solution 70% stays chemically stable in both acidic and basic environments, so most microbes can't turn it into alcohol. During high-temperature cooking, it doesn't go through Maillard burning.
Low-Calorie Health Benefits
Meet the needs of people who want better choices. It is slowly digested and has a low glycemic index. It has fewer calories than sugar but keeps the structure and bulk of sugar-free foods.
Extended Shelf Life
Guard the money you've spent on creation. The solution's antibacterial and non-reducing features help products last longer, which cuts down on waste and boosts profits.
Specifications
| Parameter | Specification |
|---|---|
| Appearance | Transparent, sweet, viscous liquid |
| Dry Solid | 69.0–71.0 % |
| Water Content | 29–31 % |
| Sorbitol Content | ≥ 70 % |
| pH Value | 5.0–7.5 |
| Relative Density (d20) | 1.285–1.315 |
| Refractive Index | 1.455–1.465 |
| Reducing Sugar | ≤ 0.21 % |
| Total Sugar | ≤ 8.0 % |
| Residual After Burning | ≤ 0.10 % |
| Heavy Metal (as Pb) | ≤ 5 PPM |
| Arsenic (as As) | ≤ 2 PPM |
| Chloride (as Cl) | ≤ 10 PPM |
| Sulphate (as SO₄) | ≤ 50 PPM |
| Nickel (as Ni) | ≤ 2 PPM |
| Ethylene Glycol | Absent/gm |
| Diethylene Glycol | Absent/gm |
| E-Coli | Absent (cfu/g) |
| Salmonella | Absent (cfu/25g) |
| Quality Assessment | Qualified with USP-NF, EP, FCC standards |
Frequently Asked Questions
Q: How does your product compare to glycerin as a humectant?
A: While both are effective polyols, our solution is more cost-effective and provides higher viscosity. Glycerin absorbs moisture slightly faster, but our product offers better value for industrial applications requiring stability and bulk.
Q: Will it crystallize during cold storage?
A: Our high-purity formulation is designed to resist crystallization in most storage conditions. When stored properly in temperatures above 15°C, crystallization risk is minimal. For extreme cold climates, we recommend storage in temperature-controlled environments.
Q: Is there a laxative effect concern?
A: Like all sugar alcohols, excessive consumption (typically over 50g per day) may cause osmotic effects. For food applications, recommended usage levels are well below this threshold. Proper labeling ensures consumer awareness.
Q: Can I use it in high-temperature processing?
A: Absolutely. Our product demonstrates excellent heat stability and doesn't undergo Maillard browning. This makes it ideal for baked goods, confectionery, and products requiring thermal processing.
Q: What's the shelf life and storage requirement?
A: The standard shelf life is 24 months when stored in cool, dry conditions in airtight containers away from direct sunlight. Optimal storage temperature range is 15°C–25°C to maintain product integrity.
Q: Do you provide technical support for formulation?
A: Yes. Our technical team offers comprehensive application guidance to help you optimize formulations for your specific products. We work closely with you to achieve desired texture, taste, and stability.
Contact Us
Ready to elevate your food production with premium Sorbitol Solution 70%? Contact us today at info@dorisfood.com